Blog
// Lekker's Blog
Dual Sourcing Metal Parts in Asia Without Killing Tooling
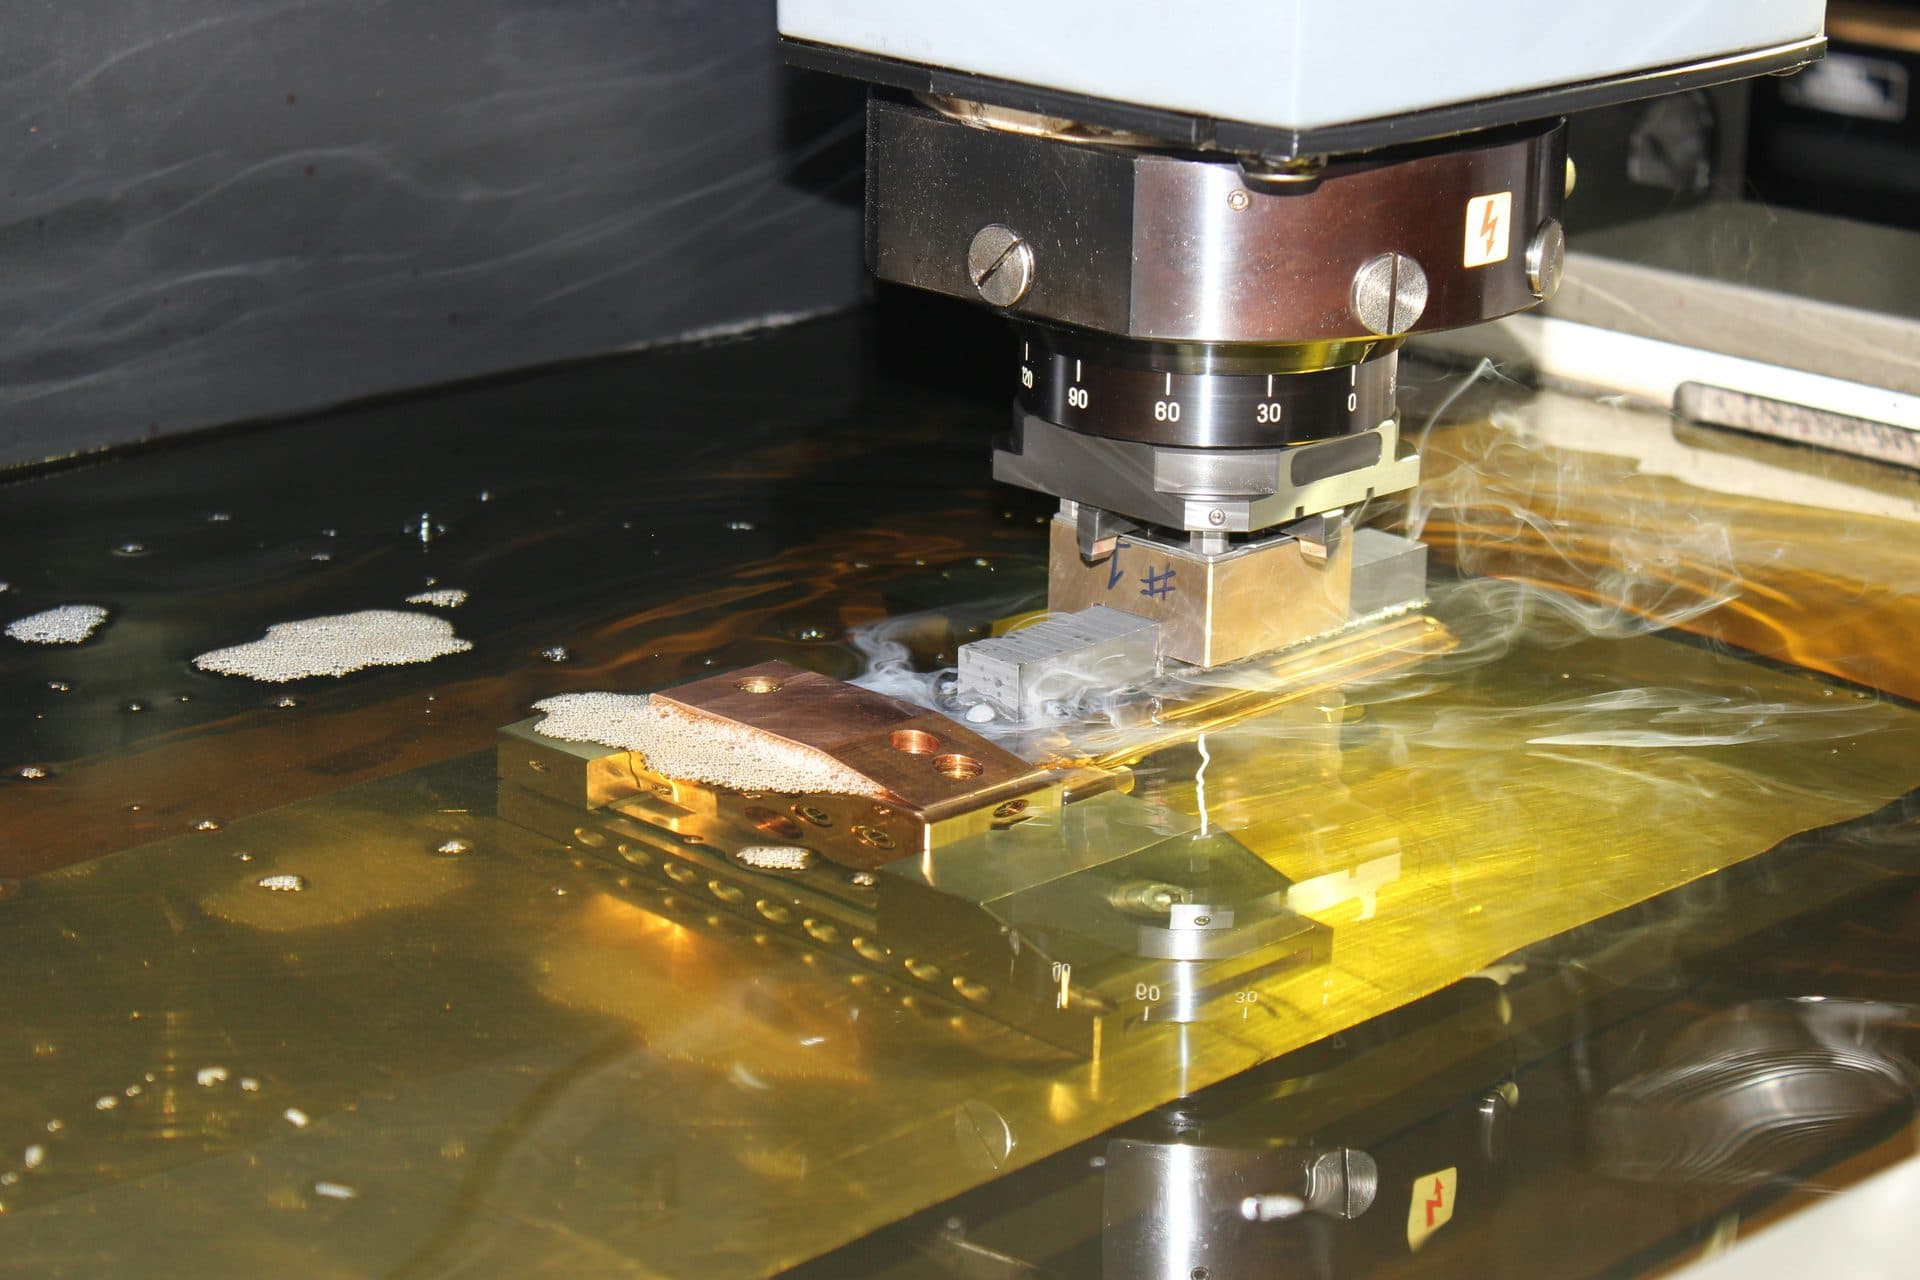
Dual sourcing in Asia for metal parts means two plants that can ship the same drawing — not one plant with a backup WhatsApp number. For sheet metal, CNC, and related fab, the hard problem is tooling and fixtures: duplicate the wrong assets and you burn cash; duplicate nothing and you never had a second source.
This guide is for buyers who already have a primary Asia (or other) fab and need a mechanical second path — including programs that split volume toward Malaysia as an Asia option. It is distinct from how to diversify your supply chain to Asia (program scope, China+1 sequencing) and from first-time supplier set-up. Here the focus is dual-source mechanics: what to copy, what to share, and how to keep tools alive.
Five rules:
1. Name what “same part” means
Before RFQs to a second plant, lock:
Drawing revision and CTQs that both plants must hit.
Material and finish callouts (including outsourced plate/paint).
Inspection method and gauge list — identical points, not “equivalent.”
Packing and labeling so lots are interchangeable in your warehouse.
Which SKUs are in scope for dual source now vs later (hero dies stay single until the boring family works).
If the second plant quotes a “similar” process with different fixtures, you are dual-sourcing a cousin, not the SKU. Write interchangeability criteria before price negotiations start.
2. Choose the tooling model deliberately
Soft dual — What you duplicate: Process knowledge; buyer-owned fixtures at both · Fits when: Stable CNC / sheet metal · Risk: Fixture cost; need identical gauges
Hard dual — What you duplicate: Two unrelated OEMs, each with fixtures · Fits when: Geopolitical or capacity shock · Risk: Two quals, two FAIs, two claim paths
Shared die / shared press tool — What you duplicate: Often not true dual · Fits when: Cast/stamp with one owned die · Risk: Single tool = single source
Plant-group second site — What you duplicate: Capacity inside one commercial group · Fits when: Overflow only · Risk: Same ownership risk
Write who pays for dies, jigs, CMM programs, and weld fixtures. If the primary “owns” everything and will not transfer, you do not have dual sourcing Asia — you have hope. Use the diversify post for program sequencing and China+1 prioritization; this table is the tool decision on each SKU family.
For castings and stamped dies, treat shared tooling as single-source until a second die exists or transfer terms are contractual. CNC and sheet-metal soft dual usually means buyer-owned fixtures and shared drawing control — cheaper than two presses, still real if gauges match.
3. Qualify the second plant on the constraint process
Do not award plant B because it is 5% cheaper on laser blanks if your constraint is weld + powder or a tight CNC bore.
Desktop + sample + process route for your revision (qualify Asia suppliers).
Compare FAI to a known-good part from plant A on the same CTQs.
Visit or audit the constraint and any critical outsourced finish (factory audit).
Confirm export packing and Incoterms language so plant B does not invent packing at first volume.
Build the second name with Market Research & Supplier Discovery when your list is thin; dual source fails when plant B is an undisclosed trader.
4. Run parallel pilots, not a flip
Keep plant A live until plant B has shipped clean lots under production intent:
Pilot volume should stress the constraint (weld distortion, thin-wall CNC, finish adhesion) — not only easy ops.
Same SQE scorecard on both: process fit, QC independence, packing, communication.
Document the volume-share rule: what delay, quality event, or capacity signal moves share from A to B (and back).
Do not freeze plant A’s tooling maintenance while “waiting to see” — dual source dies when the primary tool is neglected.
A “dual source” that only exists on a slide until the first claim is single source with marketing.
5. Protect change control across two plants
Dual sourcing dies when one plant silently tweaks a fixture or swaps a plater.
One engineering change process; both plants get the same rev package at the same time.
No unilateral material or finish substitutes.
Claim loop that can quarantine lots from either plant without freezing the other if the root cause is plant-specific.
Periodic gauge and fixture correlation so plant A and plant B do not drift apart on the same CTQ.
CNC dual-source cost notes on the site are a checklist, not a blanket price claim — use them when machining is the family you are splitting, including between Malaysia and China.
Dual sourcing metal in Asia is a tooling and control problem first, a price problem second. Define the SKU, pick the fixture model, qualify the constraint, pilot in parallel, and lock change control — or you have moved risk onto a second PO, not reduced it.